Bio-PE vs. Fossil-PE Baby Diaper Line Setup Guide | Welldone

Material Supply Resilience & Baby Diaper Line Engineering · November 18, 2026
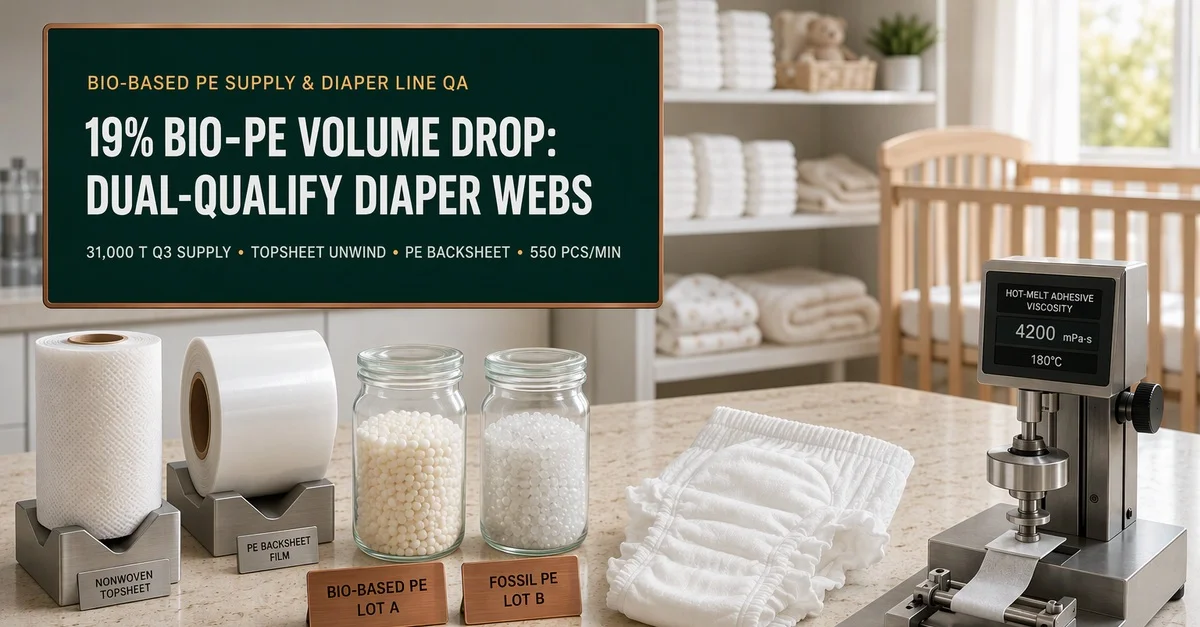
19% Bio-PE Volume Drop: Dual-Qualify Baby Diaper Topsheet & Backsheet Webs on 550–600 pcs/min Lines
When a biopolymer supplier experiences a shipment contraction or financial restructuring, hygiene factories running single-sourced "eco" bills of materials face an immediate production crisis. As reported by Nonwovens News (November 17, 2026), Brazilian producer Braskem recorded a 19% consecutive quarter drop in Q3 sales of its 'I'm green' bio-based HDPE for nonwovens—falling to 31,000 tonnes from 39,000 tonnes in Q2, and 29% below the 44,000 tonnes shipped in Q3 2025—as the company seeks a restructuring deal. On the same day, Sweden's OrganoClick AB secured a SEK 13 million loan from Almi (60-month term, 6-month grace period) to scale its biobased nonwoven binders. For B2B buyers operating baby diaper and pull-up lines, this guide translates biopolymer supply volatility into a dual-qualification protocol across unwinding, splicing, breathable backsheet tension, hot-melt lamination, and bagging.
1. November 2026 Signal: 19% Bio-PE Volume Drop & Binder Scale-Up
Retail tenders and baby care brands increasingly specify bio-attributed polyethylene in bicomponent PE/PP spunbond topsheets, microporous breathable backsheet films, and outer polybags. Yet the November 17, 2026 raw-material dispatches highlight how fragile single-source bio-resin supply chains remain. While Braskem's renewable polymer revenue held broadly steady year-on-year, physical shipments of its 'I'm green' bio-based HDPE for nonwovens contracted to 31,000 tonnes in Q3 2026, down 8,000 tonnes quarter-on-quarter and 13,000 tonnes year-on-year.
Parallel upstream shifts reinforce the same lesson. OrganoClick's SEK 13 million Almi loan supports customer launches using biobased binders, while in tissue, Tissue World Magazine reported that Metsä Tissue canceled its planned Goole, UK mill investment even as Essity committed SEK 850 million to a multi-fiber machine in Lilla Edet, Sweden. At COMPAMED 2026 in Düsseldorf (November 17, 2026), Freudenberg Performance Materials and Foshan United Medical (UMT) combined silicone-coated foam and gelling wound-care portfolios to provide multi-site supply options.
The real question is what this biopolymer volume contraction means for a factory running a 400 to 600 pcs/min baby diaper or pull-up pant line. If a converter locks machine settings around a single bio-HDPE topsheet or bio-PE breathable film grade, any shipment delay forces an emergency mid-order switch to fossil-PE or alternative binder-treated webs. Without pre-qualified HMI tension, splicing, and hot-melt recipes stored for both Lot A (bio-based) and Lot B (fossil-PE), emergency substitution causes web breaks, backsheet pinholes, and rejected packs.
2. Confirmed Facts, Data Conflicts & Supply Chain Implications
To support capital equipment and material procurement, we separate facts directly confirmed by primary disclosures from Welldone's converting engineering analysis:
- Confirmed Facts from Primary Sources (November 17, 2026): According to Nonwovens News (November 17, 2026, São Paulo), Braskem reported a 19% QoQ fall in Q3 2026 sales of 'I'm green' bio-based HDPE for nonwovens to 31,000 tonnes (down from 39,000 tonnes in Q2 2026 and 29% below 44,000 tonnes in Q3 2025), while renewable polymer revenue held broadly steady YoY as Braskem seeks a restructuring deal. In a separate November 17, 2026 Stockholm report, Nonwovens News confirmed OrganoClick AB secured a SEK 13 million Almi loan (60 months, straight-line repayment after a 6-month grace period) as a German customer launches nonwovens using its biobased binder. In Düsseldorf (November 17, 2026), Freudenberg and UMT jointly presented silicone-coated foam and gelling dressings at COMPAMED 2026.
- Welldone Converting & Supply Chain Engineering Analysis: Neither Braskem, OrganoClick, nor Freudenberg mentioned Welldone, and Welldone is not involved in their operations. The station tolerances, servo unwinding tension windows, zero-speed splicing recipes, hot-melt thermal limits, and BOM dual-qualification workflows below represent Welldone's engineering guidance for buyers of T-shape baby diaper machines, pull-up baby diaper machines, and baby diaper packing machines.
⚠ News Data Conflict Found (Cross-Source Verification Disclosure):
- Conflict 1 — Braskem 'I'm green' Q3 Shipment Volume vs. Year-on-Year Revenue Stability: Nonwovens News (November 17, 2026) reports physical Q3 shipment volume of 'I'm green' bio-based HDPE fell 19% QoQ (31,000 vs. 39,000 tonnes) and 29% YoY (vs. 44,000 tonnes in Q3 2025), whereas renewable polymer revenue held broadly steady YoY. Steady supplier revenue does not guarantee physical resin availability on spot markets; converters must secure dual-qualified backup rolls.
- Conflict 2 — Welldone Baby Diaper Product Page Generic Header Text vs. Dedicated Model Details Table: On Welldone's website, the generic header paragraph on both the T-shape baby diaper page (
WD-NK-500T-HSV/WD-BDM-013) and the baby diaper packing machine page (WD-BDPM-012) repeats a template string ("High speed 600 pcs per minutes diaper manufacturing machine"). However, the dedicatedDetailstable on the T-shape page specifiesDesign speed: 500pcs/minandStable speed: 400pcs/min, while the pull-up baby pants page (WD-NK-600L-SV/WD-BDM-012) specifiesDesign speed: 600pcs/minandStable speed: 500-550pcs/min(bothPassing rate ≥ 98%,Waste Rate < 2%). Always anchor FAT contracts to the dedicated model specification table.
3. 8-Layer Dual-Qualified Baby Diaper Web Architecture

Where exactly does bio-based polyethylene sit inside a modern baby diaper or pull-up pant, and which converting stations feel the impact when a converter switches between bio-PE and conventional fossil-PE rolls? As shown in Figure 1, eight functional web and core zones interact on the production line:
- Layer 1 — Hydrophilic Spunbond or Through-Air Bonded Topsheet (14–18 g/m²): Premium eco diapers frequently use bicomponent PE/PP sheath-core fibers where the outer sheath is bio-based HDPE for skin softness and low thermal bonding temperatures, while standard lots use 100% polypropylene spunbond.
- Layer 2 & Layer 3 — Acquisition-Distribution Layer (ADL, 25–40 g/m²) & Transfer Sub-Layer: Moves liquid rapidly downward. When converters test biobased-binder airlaid or carded webs (such as grades enabled by OrganoClick's binder chemistry) alongside resin-bonded PET/PP ADLs, wet stiffness and rotary die-cutting dust change significantly.
- Layer 4 & Layer 5 — Channeled Fluff Pulp + SAP Core & Core Wrap Sheet (12–16 g/m²): Defibrated wood pulp and high-gel SAP encapsulated in wet-strength tissue or ultralight SMS nonwoven.
- Layer 6 — Breathable Microporous PE Backsheet Film (16–22 g/m²): Extruded from linear low-density and high-density polyethylene stretched around calcium carbonate filler. Switching between bio-attributed PE film and standard fossil-PE film alters machine-direction (MD) modulus and thermal shrinkage.
- Layer 7 & Layer 8 — Hydrophobic Leg-Cuff Barrier Nonwovens, Cloth-Like Outer Nonwoven & Frontal Tape System: Laminated to the PE backsheet film via fine-grammage hot-melt adhesive spiral or slot-coat spray.
4. Four Converting Failures During Emergency Web Lot Switching
A common mistake is assuming that because bio-based HDPE is chemically identical to fossil HDPE at the monomer level, roll-to-roll converting performance on a 550 pcs/min diaper line will be identical across different compounders. Switching between a bio-PE roll (Lot A) and a backup fossil-PE or alternative binder roll (Lot B) without changing machine settings triggers four failure modes:
- Failure Mode 1 — Zero-Speed Splicing Tail Snap on Topsheet Unwinders: Bicomponent PE/PP topsheets with bio-HDPE sheaths exhibit a different coefficient of friction (COF) and lower yield point than homopolymer PP spunbond. When the automatic splicer fires at 500–550 pcs/min and accelerates the new roll from zero speed through the festoon dancer, an unadjusted braking ramp snaps the incoming web within 20 meters of the splice tape.
- Failure Mode 2 — Breathable PE Backsheet Neck-In & Print Misregistration: Microporous breathable PE films compounded from different resin batches vary in CaCO3 dispersion and MD orientation. A 15% lower secant modulus causes the 16–22 g/m² film to neck-in by 3–6 mm under standard tension, exposing sticky construction glue along the chassis edge and shifting eye-mark registration beyond ±1.5 mm.
- Failure Mode 3 — Hot-Melt Adhesive Burn-Through on Cloth-Like Backsheet Lamination: When laminating breathable PE film to the outer cloth-like nonwoven, construction glue is sprayed at 150°C–165°C. If a substitute bio-PE film lot has a lower thermal relaxation threshold, excessive glue temperature or nip pressure creates microscopic pinholes.
- Failure Mode 4 — End-of-Line Polybag Seal Wrinkles & Leakers: On automatic diaper baggers running PE polybags, switching between bio-PE and conventional LDPE/HDPE bagging films shifts the heat-sealing window by 4°C–8°C, causing weak cold seals or over-melted seal strings.
Illustrative Example Only (Unplanned Roll-Switch Downtime Impact):
Consider an illustrative scenario on a full-servo pull-up baby diaper line operating at its verified stable speed of 500 pcs/min. If an uncalibrated mid-shift switch from a delayed bio-PE backsheet roll to an unprofiled fossil-PE backup roll causes 4 web-break and glue-cleanup stops per 8-hour shift (15 minutes per stop = 60 minutes lost), the line loses 30,000 saleable pants per shift plus ~1.2% startup splice waste. Pre-storing dual-lot HMI tension and hot-melt recipes eliminates this changeover penalty. (Note: Illustrative calculation only; not a customer case study or financial guarantee.)
Consider an illustrative scenario on a full-servo pull-up baby diaper line operating at its verified stable speed of 500 pcs/min. If an uncalibrated mid-shift switch from a delayed bio-PE backsheet roll to an unprofiled fossil-PE backup roll causes 4 web-break and glue-cleanup stops per 8-hour shift (15 minutes per stop = 60 minutes lost), the line loses 30,000 saleable pants per shift plus ~1.2% startup splice waste. Pre-storing dual-lot HMI tension and hot-melt recipes eliminates this changeover penalty. (Note: Illustrative calculation only; not a customer case study or financial guarantee.)
5. Station Focus I: Topsheet Nonwoven Servo Unwinding & Zero-Speed Splicing

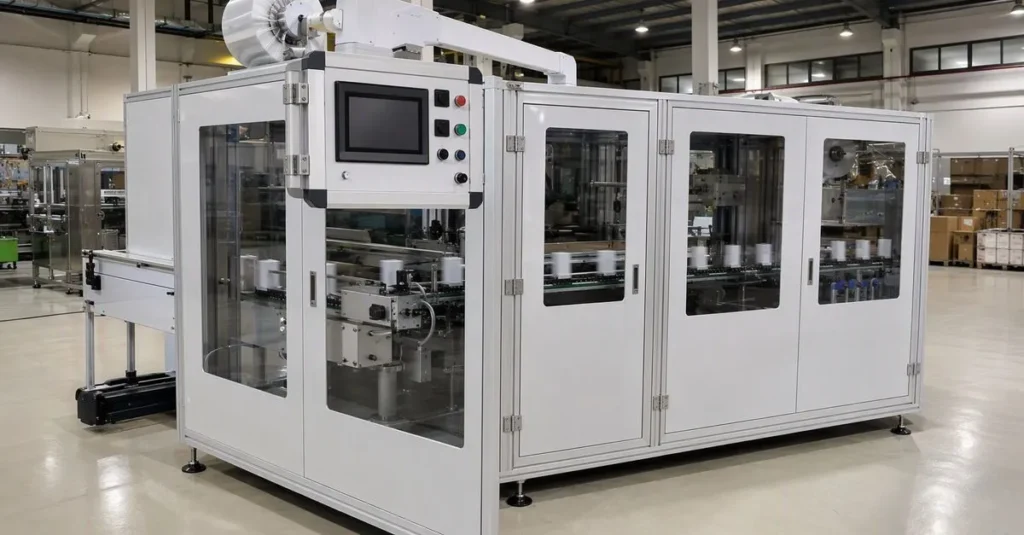
To dual-qualify a bicomponent bio-PE/PP topsheet alongside a conventional spunbond topsheet—or run biobased-binder ADL webs—the unwinding and splicing module must isolate the main drum from roll-inertia spikes. As shown in Figure 2, the topsheet unwinder integrates dual servo spindles, a pneumatic zero-speed splicing head, and a multi-pass festoon accumulator. When qualifying two suppliers on a T-shape baby diaper machine (400 pcs/min stable speed) or a pull-up baby diaper machine (500–550 pcs/min stable speed), engineers lock three HMI settings:
- Continuous Diameter-Tapered Torque Control: An ultrasonic roll-diameter sensor tracks the parent roll from 1,000 mm down to the 76 mm core, reducing servo torque proportionally so web tension stays within ±0.3 N.
- Lot-Specific Dancer Pressure Curves: Store Preset A for softer bio-PE bicomponent webs (12–16 N web tension) and Preset B for higher-modulus standard PP spunbond webs (16–22 N), selectable on the Mitsubishi or Siemens HMI.
- Synchronized Splicing Ramp Window: During zero-speed splicing, the festoon buffer feeds the line for 0.8–1.2 seconds while the standby spindle accelerates along an S-curve ramp, preventing tail snap on 14–15 g/m² webs.
6. Station Focus II: Breathable PE Backsheet Tension & Neck-In Control
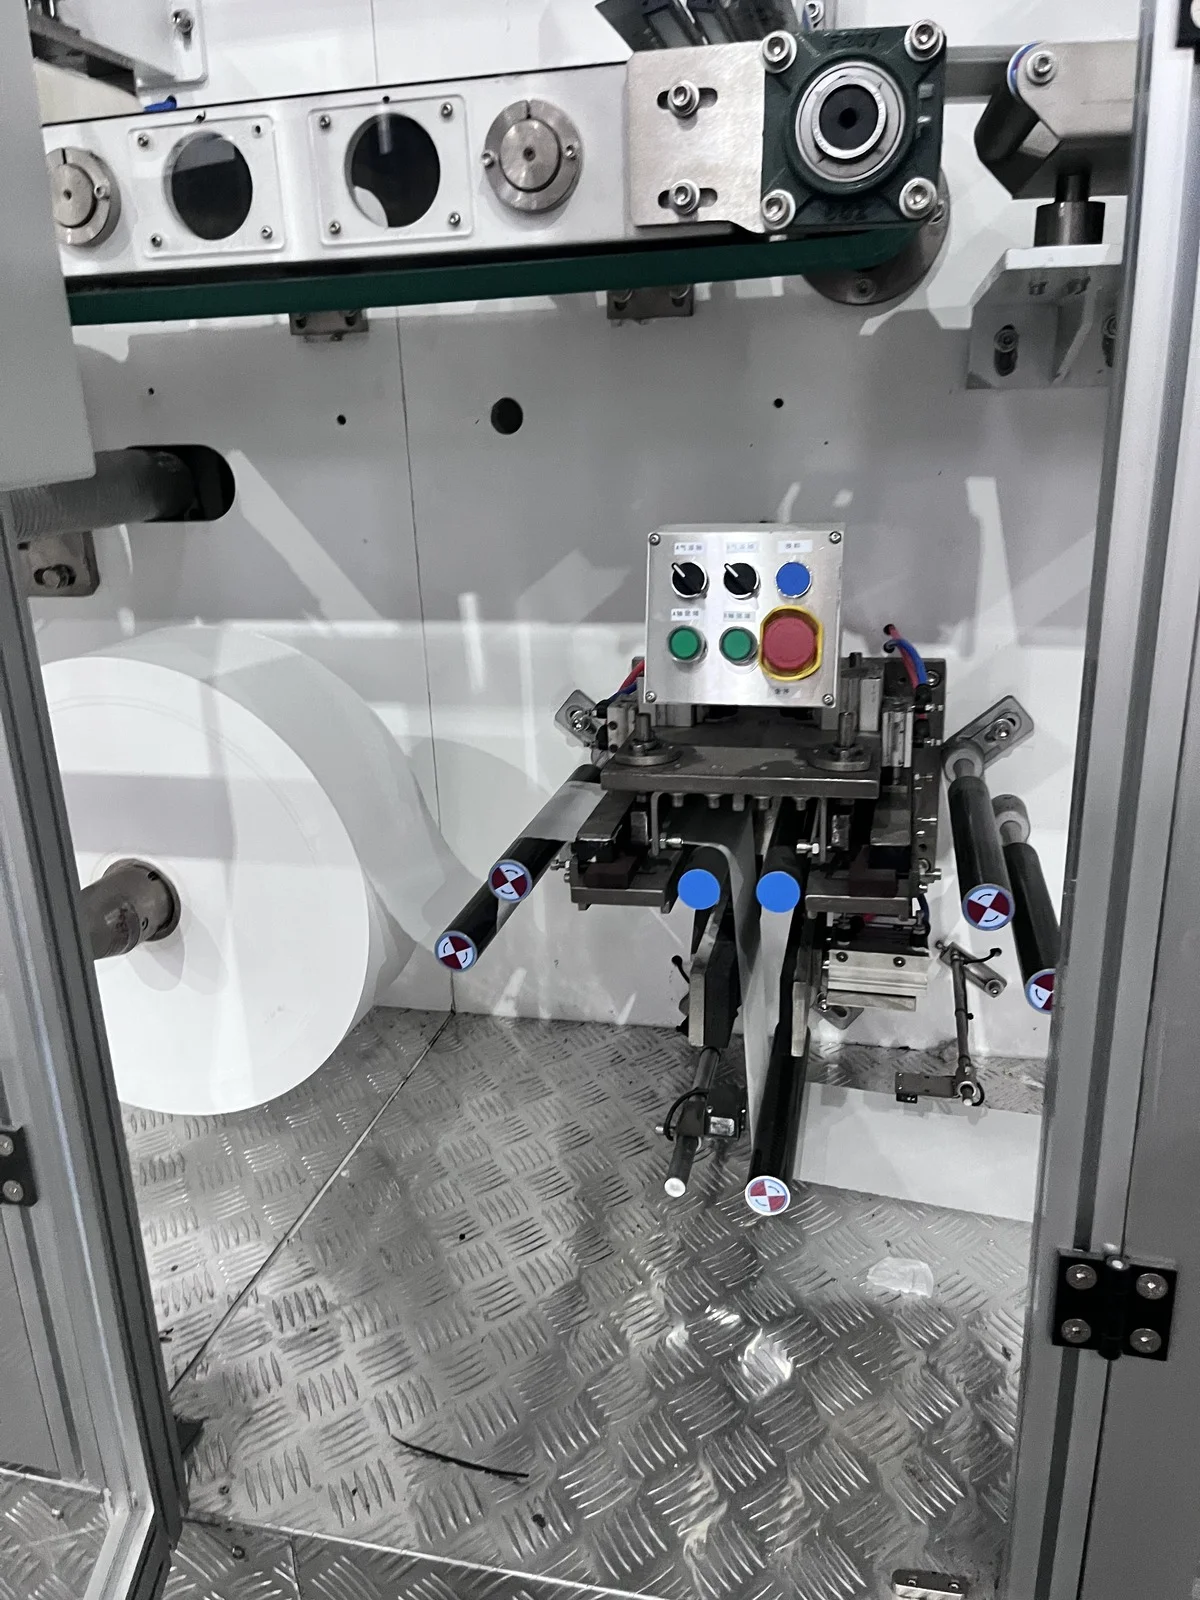
Breathable polyethylene backsheet film is the most tension-sensitive substrate on a diaper line. Because microporous PE film achieves breathability by stretching a CaCO3-filled polymer matrix, minor variations in bio-HDPE blending ratios or fossil LLDPE/HDPE grades alter elastic recovery. As illustrated in Figure 3, Welldone's PE backsheet station pairs servo-driven unwind spindles with low-friction idler rollers, curved spreader rolls, and closed-loop web guiding (Chinese cost-effective or BST web guides):
- Keep MD Elongation Under 1.5%: Calibrate unwinder dancer feedback so running film elongation stays within 1.0%–1.5%, keeping cross-direction shrinkage within ≤ 1.5 mm across a 200–320 mm diaper web.
- Active Print Eye-Mark Phase Correction: For printed backsheets, the servo draw roller reads eye-mark pitch on every diaper length and adjusts phase dynamically across bio-PE and fossil-PE lots.
7. Station Focus III: Cloth-Like Backsheet Lamination & Hot-Melt Thermal Windows

Once the breathable PE film leaves the unwinder, it enters the cloth-like backsheet lamination station (Figure 4) to bond with an outer hydrophobic spunbond nonwoven. In most cases, pinhole leaks and delamination after a raw-material switch trace back to unadjusted hot-melt lamination parameters. Whether using a Chinese cost-effective glue machine or an optional Nordson system, dual-qualifying bio-PE and fossil-PE backsheets requires locking three variables:
- Low-Temperature Spiral Spray Window (140°C–152°C): Dropping applicator head temperature by 5°C–8°C and keeping a 25–35 mm nozzle-to-web gap lets adhesive filaments cool slightly before contacting 16 g/m² PE film, preventing thermal burn-through.
- Speed-Slaved Gear Pump Dosing (1.2–2.2 g/m²): The glue pump tracks main line speed (150 to 550 pcs/min) so adhesive add-on stays uniform during splicing ramps.
- Balanced Lamination Nip Pressure: A pneumatic silicone-to-steel nip bonds the outer nonwoven to the PE film at 0.15–0.25 MPa, achieving 180° peel strength of ≥ 1.2 N/25 mm without crushing micro-pores.
8. End-of-Line Sync: Polybag Sealing Recipes for Bio-PE & Fossil-PE Films
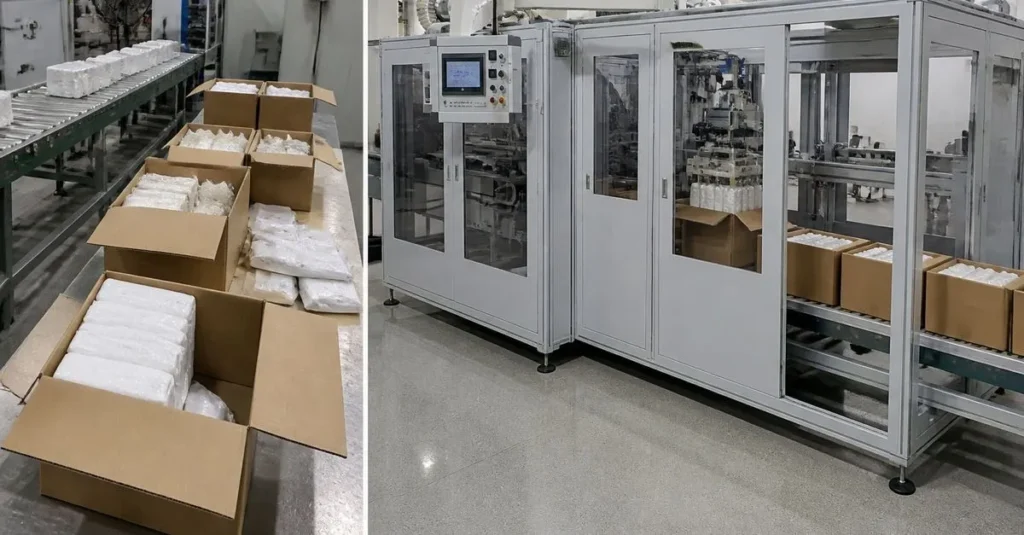
Many brands pair bio-based LDPE/HDPE polybags with bio-PE backsheets. On a Welldone baby diaper packing machine (WD-BDPM-012, PE poly bag, < 2% waste rate), switching between bio-PE and fossil-PE bagging films requires dual PLC sealing-jaw temperature presets (+5°C offset) to prevent gusset splitting on S/M/L/XL stacks.
9. Engineering Matrix: Dual-Qualification Parameters Across Diaper Stations
Lock machine recipes for both bio-based PE (Lot A) and fossil-PE (Lot B) webs during FAT:
| Converting Station & Web Layer | Bio-PE / Biobased-Binder Web Risk (Lot A) | Fossil-PE Switchover Risk (Lot B) | Welldone Machine & HMI Control Solution | FAT / Incoming QA Target Metric |
|---|---|---|---|---|
| Topsheet Unwinder & Auto Splicer (14–18 g/m²) | Lower sheath softening point & higher surface friction during splice acceleration | Higher tensile modulus causes splice tape peel if dancer pressure is too low | Servo diameter-tapered unwind + dual HMI tension recipes (12–16 N vs. 16–22 N) | 10 consecutive auto-splices at 400–550 pcs/min with 0 web breaks |
| ADL Unwinder & Rotary Cutter (25–40 g/m²) | Biobased-binder or cellulose-blend ADL generates fine lint at rotary anvil | Resin-bonded PET/PP ADL changes spring-back thickness under transfer vacuum | Tungsten-carbide rotary knife + localized dust suction manifold & vacuum damper | Clean cut edge (≤ 0.5 mm fuzz) & placement accuracy ± 1.5 mm |
| Breathable PE Backsheet Unwinder (16–22 g/m²) | Batch-to-batch CaCO3 & bio-HDPE variation triggers 3–6 mm CD neck-in | Different MD stretch ratio shifts printed backsheet eye-mark registration | Closed-loop dancer feedback (≤ 1.5% elongation) + active eye-mark servo phase | CD width shrinkage ≤ 1.5 mm; print registration ± 1.5 mm |
| Cloth-Like Backsheet Hot-Melt Lamination | Thermal pinholes or film puckering if construction glue exceeds 155°C | Insufficient bond peel strength if nip pressure is not matched to film stiffness | Speed-slaved gear pump (1.2–2.2 g/m²) + 140–152°C spiral spray & pneumatic nip | Lamination peel strength ≥ 1.2 N/25 mm; 0 hydrostatic pinholes |
| Automatic Polybag Packing Machine (WD-BDPM-012) | Bio-PE polybag film requires narrower heat-sealing temperature window | Cold-seal splitting on gussets under high-compression stack bagging | Servo counting/stacking + dual PLC sealing-jaw temperature & dwell presets | Neat bag seal integrity ≥ 98% passing rate; < 2% packaging waste |
10. How Welldone Supports Baby Care Machinery, BOM Materials & Finished Supply
When upstream resin markets tighten—as highlighted by Braskem's 19% quarterly volume drop—a diaper manufacturer's profitability depends on both machine adaptability and raw-material security. I believe locking a baby diaper line to a single-source specialty resin without pre-validated backup webs is an avoidable risk; dual-qualifying machine recipes and material supply during commissioning protects utilization year-round.
Operating since 2008 and incorporated in 2013, JINJIANG WELLDONE MACHINE CO., LTD. supports global hygiene partners across three scopes:
- Full-Servo Baby Care Converting & Packing Lines: We manufacture T-shape baby diaper machines (
WD-NK-500T-HSV, 500 pcs/min design, 400 pcs/min stable speed), pull-up baby diaper machines (WD-NK-600L-SV, 600 pcs/min design, 500–550 pcs/min stable speed), and baby diaper packing machines (WD-BDPM-012), with Mitsubishi or Siemens PLC/servo control, Nordson or Chinese glue systems, and BST or custom web guides. - Matched Hygiene Raw Material & Dual-Lot BOM Support: Welldone supplies matched raw materials—topsheets, breathable PE backsheets, ADL, fluff pulp, SAP, spandex, tapes, and hot-melt adhesives—pre-tested during FAT so you have verified primary and backup BOM lots ready.
- Finished Hygiene Products Supply: We also coordinate supply of finished baby diapers, baby pull-up pants, adult incontinence products, sanitary pads, and underpads. Specific grades, MOQs, and terms are confirmed via inquiry.
11. 8-Step Buyer & Factory Actionable Qualification Checklist
Before signing a supply contract for diaper webs or conducting Factory Acceptance Testing (FAT), execute this 8-step checklist:
- Freeze a Dual-Source BOM Sheet: Specify both Primary Lot A (bio-PE or biobased-binder web) and Backup Lot B (fossil-PE/PP web) with identical roll widths and 76 mm cores.
- Audit MD Secant Modulus & COF on COA: Require suppliers to report MD elongation at 5 N/25 mm load and surface COF alongside basis weight (g/m²).
- Run Back-to-Back Zero-Speed Splicing Trials in FAT: Splice Lot A into Lot B 10 consecutive times at stable speed (400 pcs/min T-shape; 500–550 pcs/min pull-up) with zero breaks.
- Measure Breathable Backsheet Neck-In Across Roll Depletion: Verify cross-direction film shrinkage stays ≤ 1.5 mm from 1,000 mm OD to 100 mm OD.
- Map the Hot-Melt Lamination Thermal Window: Lock the spiral-spray window (140°C–152°C, 1.2–2.2 g/m²) achieving ≥ 1.2 N/25 mm peel strength with 0 pinholes under a 200 mm hydrostatic head.
- Verify Printed Backsheet Eye-Mark Phase Recovery: Confirm ± 1.5 mm print registration recovery within 3 pads after an automatic splice.
- Store Named Multi-Lot Recipes in PLC/HMI: Save one-touch presets (
LOT_A_BIO_PEandLOT_B_FOSSIL_PE) for tension, dancer pressure, glue dosing, and bagger sealing. - Clarify Dedicated Model Speeds & End-of-Line Scope: Confirm whether your contract specifies a 400 pcs/min T-shape or 500–550 pcs/min pull-up line, and note that website packing pages cover primary polybagging (
WD-BDPM-012); request custom secondary case packing via direct consultation.
If your bio-PE supplier cut quarterly volume by 19% next month, could operators switch to a backup roll in three minutes via a saved HMI recipe?
12. Source & Date Verification
- Primary Raw-Material Supply Source (November 17, 2026): Nonwovens News (Haydn Davis, São Paulo) — I'm Green volumes fall as Braskem seeks restructuring deal (Q3 2026 bio-based HDPE sales down 19% QoQ to 31,000 tonnes vs. 39,000 tonnes in Q2 2026 and -29% YoY vs. 44,000 tonnes in Q3 2025).
- Secondary Raw-Material Source (November 17, 2026): Nonwovens News (Haydn Davis, Stockholm) — OrganoClick loan supports biobased binder scale-up (SEK 13 million 60-month Almi loan with 6-month grace period).
- Auxiliary Medical/Hygiene Material Source (November 17, 2026): Nonwovens News (Düsseldorf) — Freudenberg and UMT combine wound-care material portfolios at COMPAMED 2026.
- Auxiliary Tissue Investment Sources (November 2026): Tissue World Magazine — Metsä Tissue cancels tissue mill investment in Goole, UK & Essity invests in new TM to boost Tork production at Lilla Edet.
13. Frequently Asked Questions (FAQ)
1. Can one Welldone baby diaper line run both bio-PE and fossil-PE webs without hardware changes?
Yes. On Welldone full-servo T-shape and pull-up baby diaper machines, both web types share the same unwinders and nips via pre-saved HMI recipes.
2. Why do breathable PE backsheet films neck-in across different resin lots?
Variations in HDPE/LLDPE melt index or bio-resin blending shift film modulus. Closed-loop servo unwinding caps MD elongation below 1.5% so CD shrinkage stays within ≤ 1.5 mm.
3. How do we prevent hot-melt glue burn-through on 16–18 g/m² bio-PE backsheet films?
Use a speed-slaved gear pump applying 1.2–2.2 g/m² via spiral spray at 140°C–152°C with a 25–35 mm nozzle gap.
4. Can Welldone supply dual-qualified diaper raw materials or finished baby diapers alongside the line?
Yes. Alongside converting and packing machines, Welldone supplies matched raw-material BOMs and finished diapers via our official inquiry page.
14. Request a Baby Diaper Line Configuration or BOM Trial Consultation
Planning to commission a baby diaper line, dual-qualify bio-PE and fossil-PE BOMs, or source finished products? Contact Welldone via our official contact page:
Website: www.cnwelldone.com | Email: welldone@cnwelldone.com