Full Servo vs Semi Servo Sanitary Napkin Machine | Welldone

Full Servo vs Semi Servo for Sanitary Napkin Lines: Which Configuration Should You Specify?
Two quotations for a sanitary napkin line sit in your inbox. One says full servo. The other says semi servo. The price gap is large enough to be uncomfortable.
If you cannot say what that gap is actually buying, you are negotiating against a label. The word "servo" appears in both quotations, but it describes different things in each one.
Starting a Sanitary Napkin Manufacturing Business · Part 3
Part 1: Which line to start with — pad vs liner vs menstruation pant.
Part 2: Define the product first — the specification checklist before requesting a quote.
Part 3 — this article: full servo vs semi servo for sanitary napkin lines.
Part 4: Can one machine produce both pads and liners?
Part 1: Which line to start with — pad vs liner vs menstruation pant.
Part 2: Define the product first — the specification checklist before requesting a quote.
Part 3 — this article: full servo vs semi servo for sanitary napkin lines.
Part 4: Can one machine produce both pads and liners?
What "servo" actually changes on a sanitary pad line
Actually, the price difference between a full-servo and a semi-servo sanitary napkin line traces to one engineering decision: whether each unwinding and forming station runs its own closed-loop motor, or whether those stations share a mechanical heartbeat from a central main shaft.
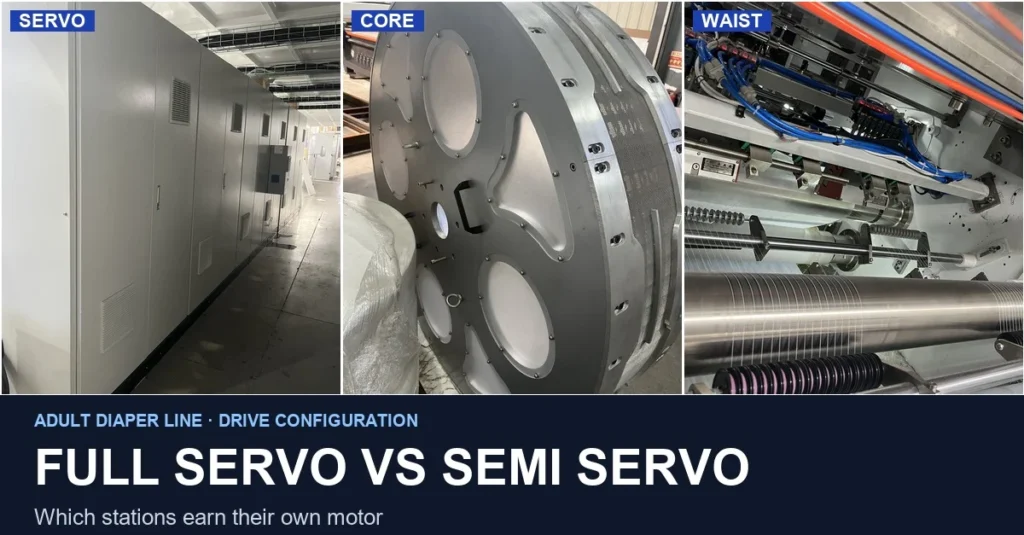
In a full-servo line, every key section — topsheet unwinder, core forming unit, wing former, cutter — has its own motor that knows where it is and can adjust independently. In a semi-servo line, the servo motors drive the key sections while cams and gears transmit motion to the rest. The machine still runs. The difference is where the precision lives and how the line responds when something varies — a thinning roll, a core weight tolerance at the edge of spec, a wing fold that drifts on the third shift.
Not speed. Control.
The three drive systems at a glance
| Drive system | Design speed | Stable speed | Positioning | Best for |
|---|---|---|---|---|
| Full-Servo | 1200 pcs/min | 1000 pcs/min | ±0.02 mm | High-end winged pads, ultra-thin, panty liners |
| Semi-Servo | ~1000 pcs/min | 850–900 pcs/min | ±0.05 mm | Standard sanitary pads and panty liners |
| Fully Mechanical | ~800 pcs/min | 750 pcs/min | ±0.1 mm | Entry-level, local-market brands |
Source: Welldone /all-female-care-machines product specification page. Design speeds and best-fit categories are as stated in the drive-system descriptions on that page.
The stations that genuinely need their own motor
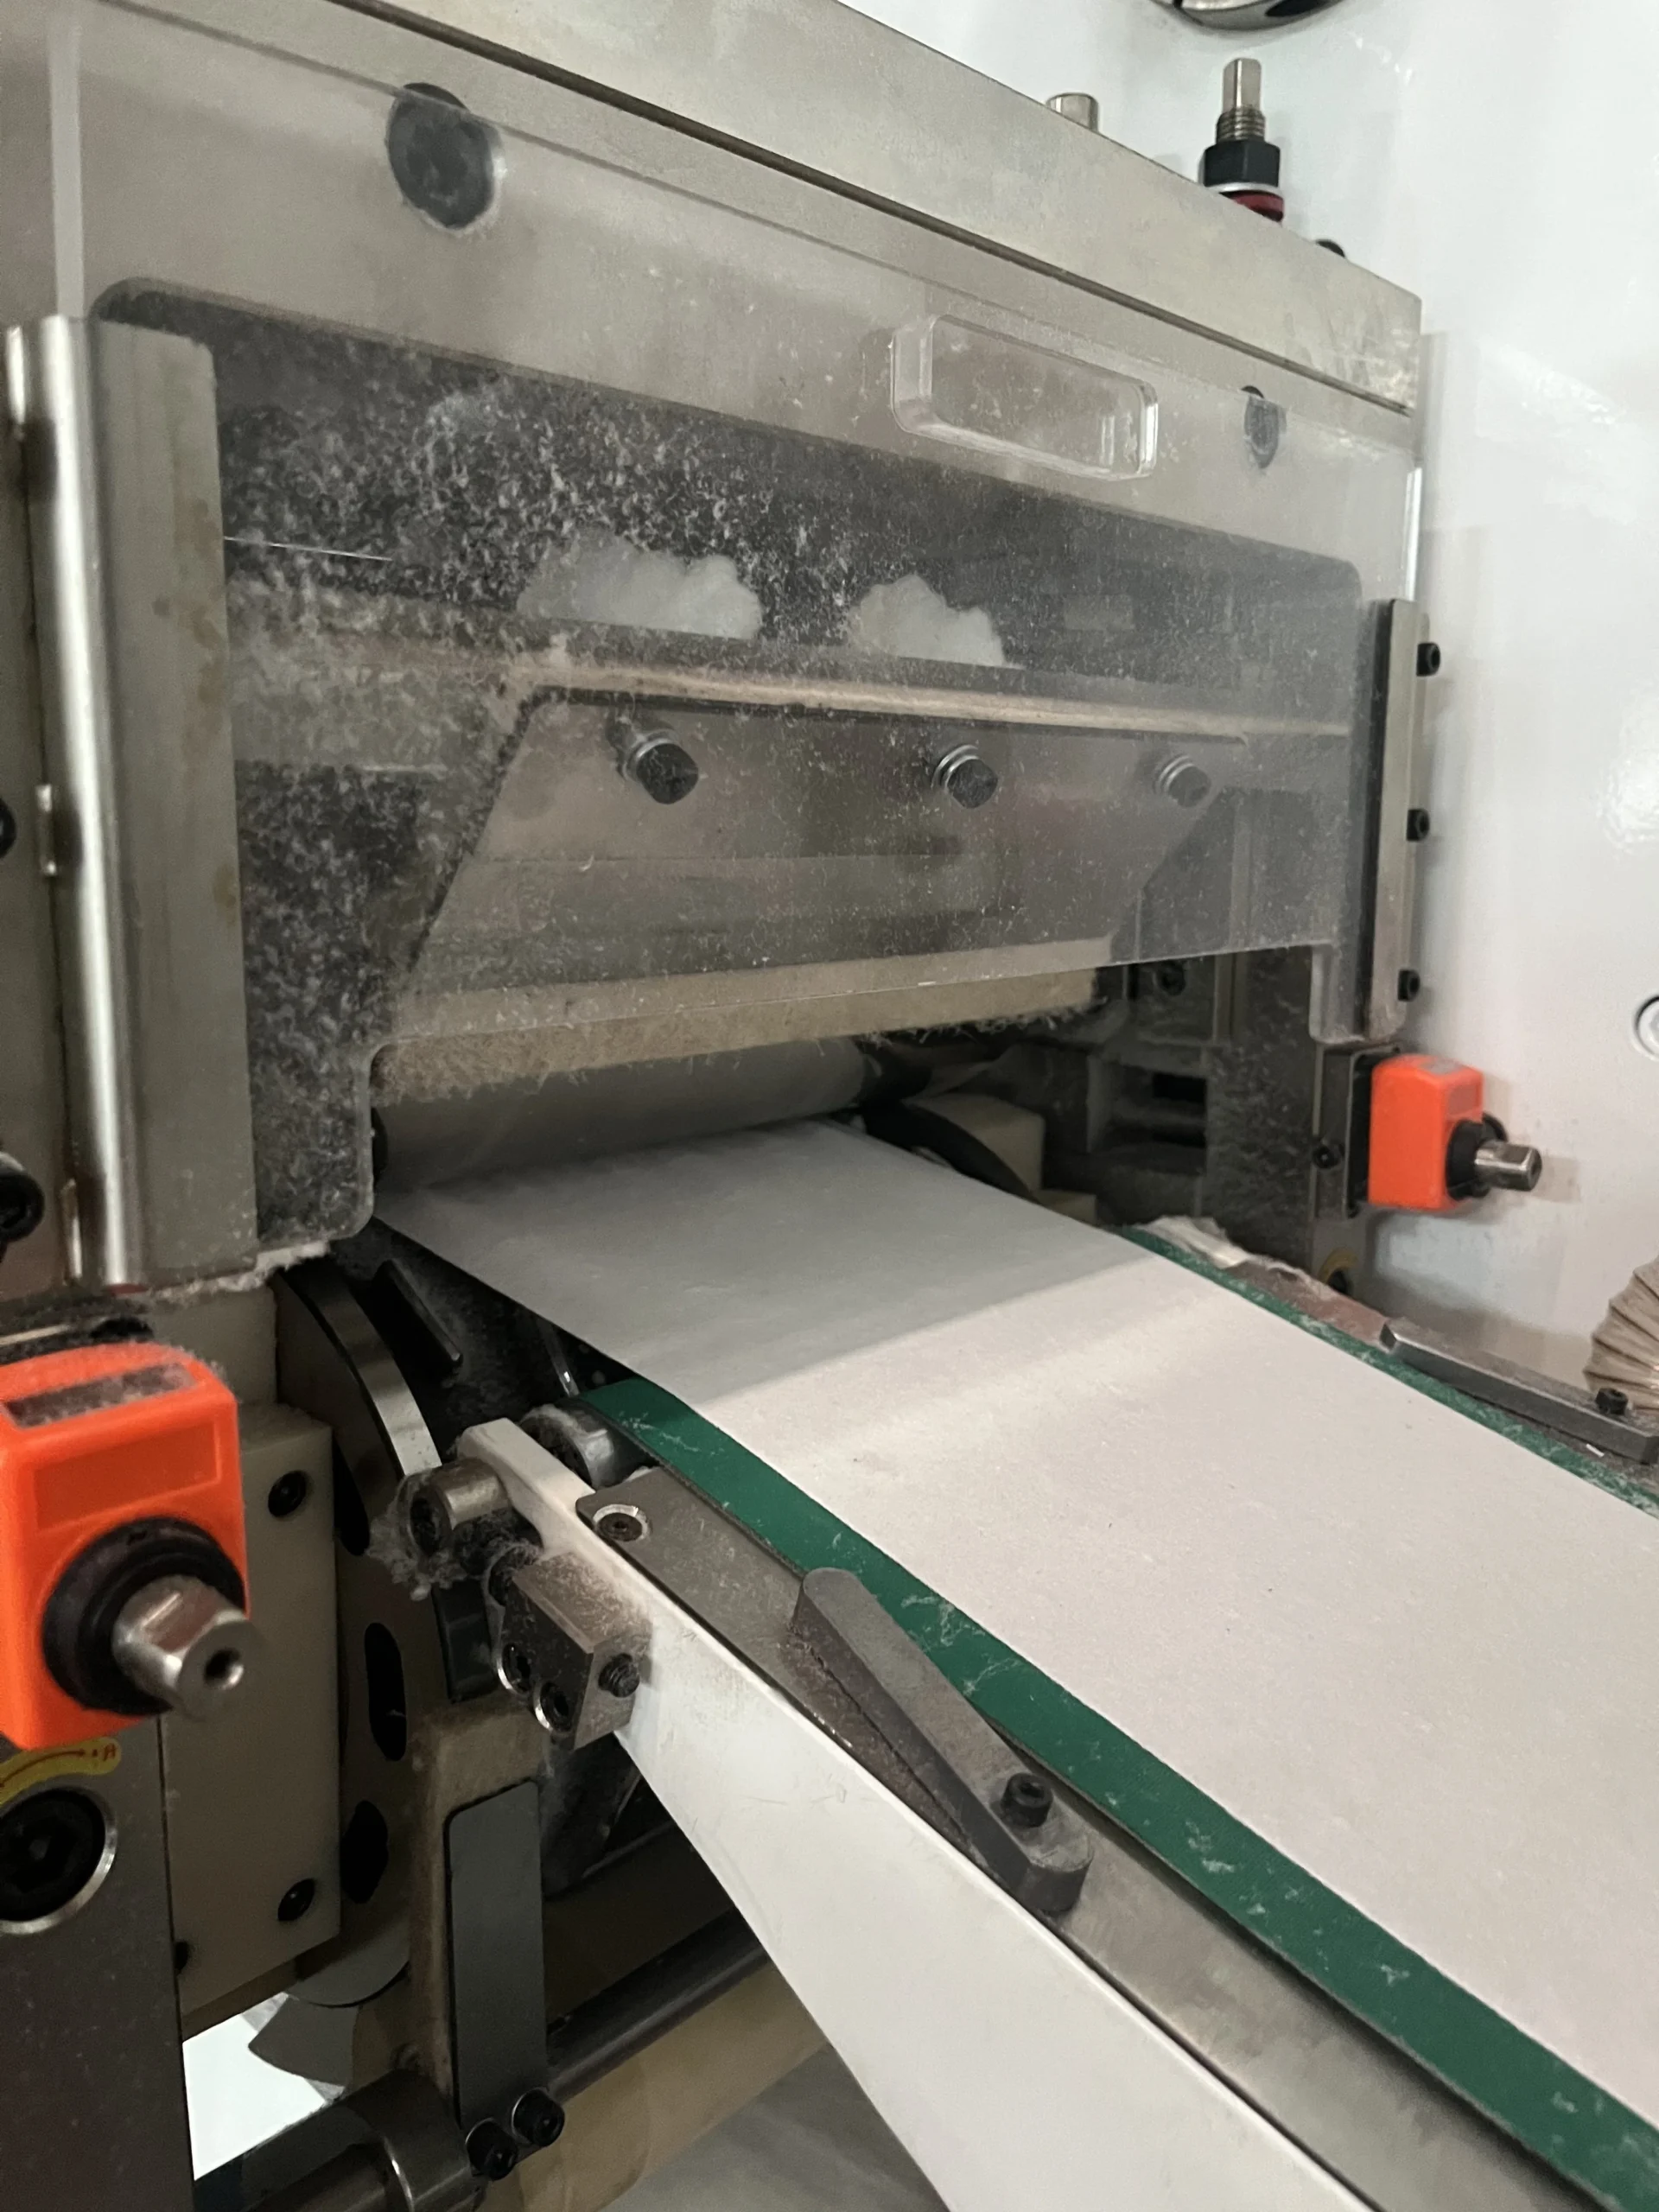
Full-servo on a sanitary napkin line means independent servo motors for each unwinder and forming station. The three that matter most are wing forming, core positioning and — on menstruation pant lines — ultrasonic sealing.
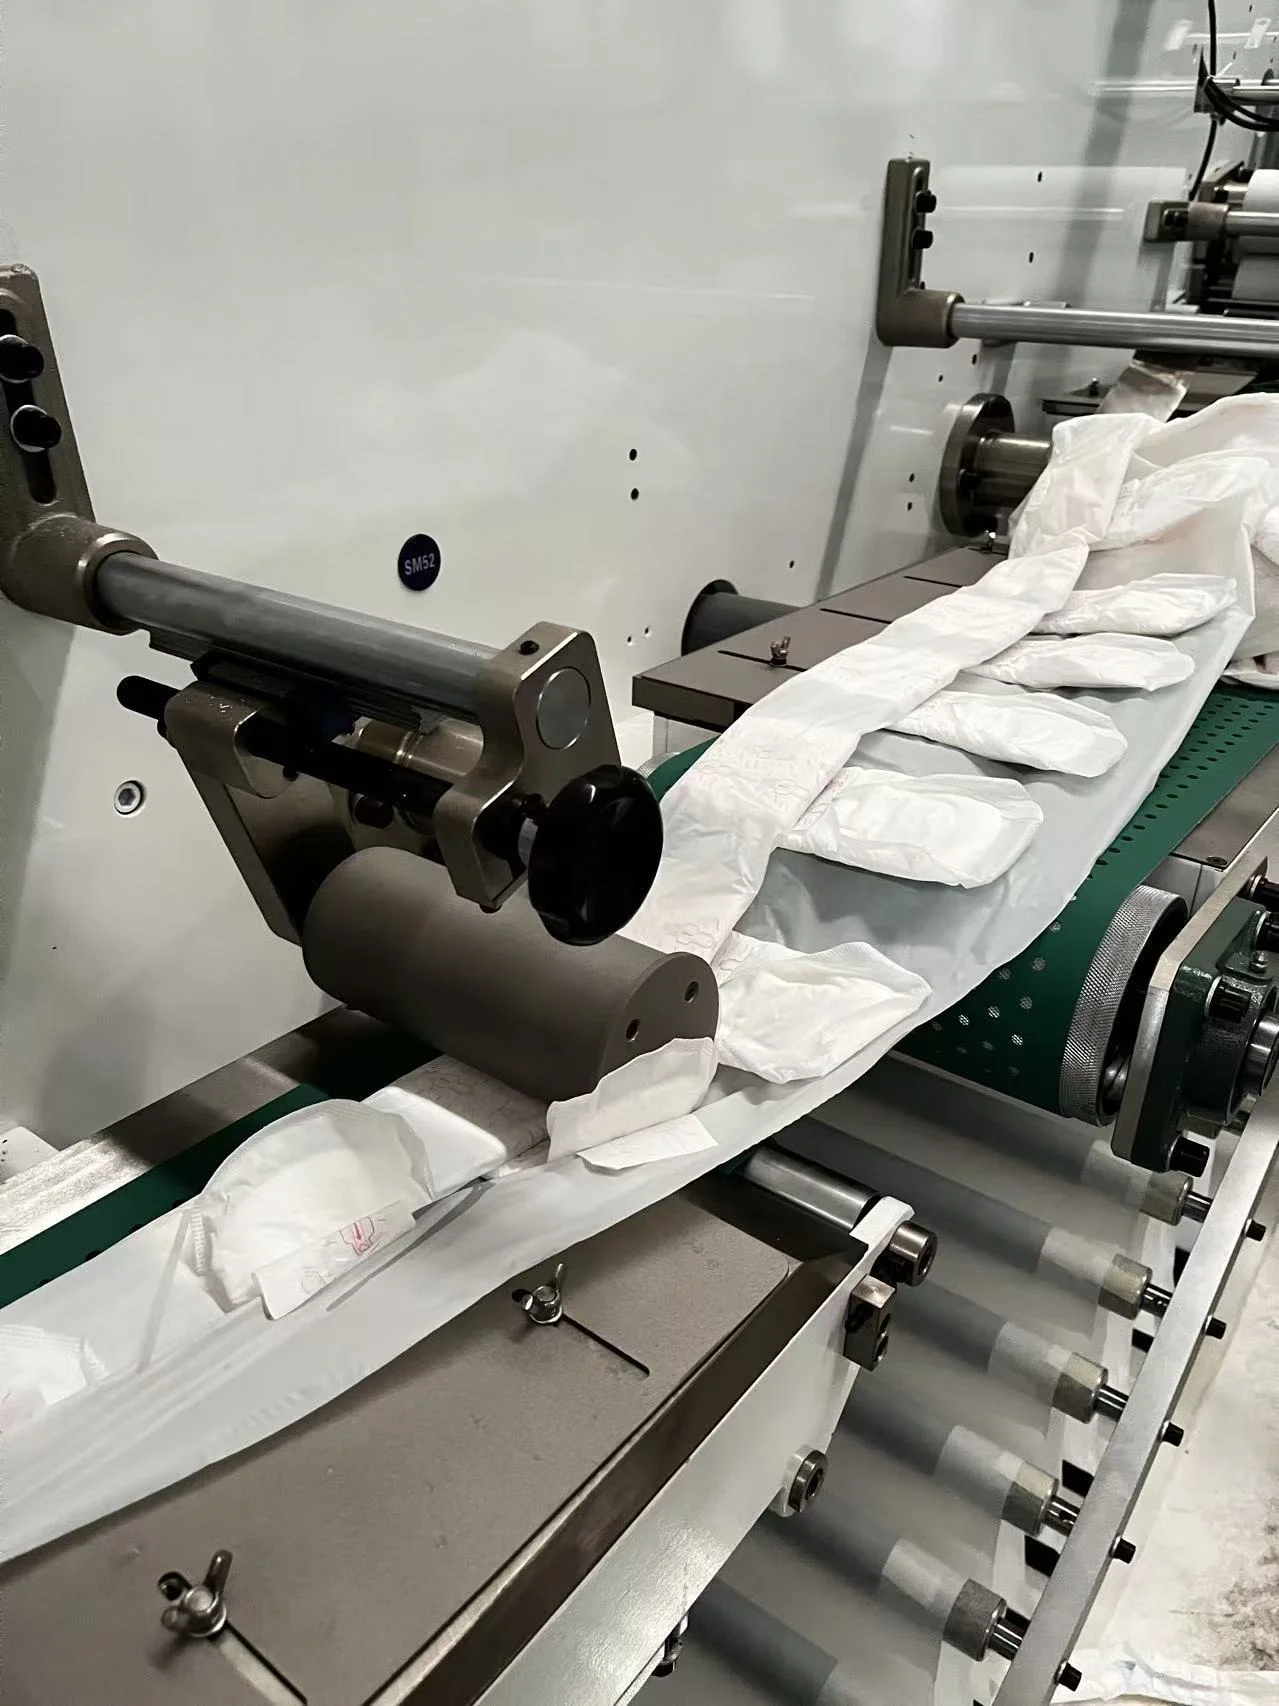
Wing forming applies folded side wings to the pad body. The fold angle and bond position must stay consistent within tight tolerances. A servo-driven wing former adjusts tension per recipe and re-profiles when the size changes. A mechanical cam drives the fold at a fixed geometry; changing it means a cam swap.
Core positioning places the formed absorbent core on the backsheet web within fractions of a millimetre. At 1000 pcs/min the core lands on the web roughly 17 times per second. At ±0.02 mm positioning accuracy, the core sits where it should every time. At ±0.1 mm, a batch at the tolerance edge shows as pad-to-pad absorbency variance — something a consumer notices before your QC team does.
What the main shaft still handles well
A semi-servo line is not a worse line. It is a differently architected line. The main shaft carries the motion for sections where mechanical consistency is reliable: general conveying, basic lamination, and length-stable transport between stations.
The servo motors on a semi-servo line go where variance matters most — the core forming and one or two other stations — and the cam-gear transmission handles the rest. At 850-900 pcs/min stable on a standard flat pad, the mechanical sections do not introduce problems. The issue arises when the product asks more of those stations: a thin core that needs tighter SAP dosing tolerance, a wing that varies in fold geometry across sizes, or a high-speed run at the edge of the mechanical envelope.
The precision numbers: ±0.02 vs ±0.05 vs ±0.1 mm
These three numbers describe how far a station can drift from its target position before the drift shows in the product. The practical meaning differs by station.
On the unwinder, ±0.1 mm tension variance shows up as splice failures near end-of-roll, where the thinner remaining material is less forgiving. On core forming, ±0.1 mm shows up as core shift — the absorbent pad sits slightly off-centre inside the backsheet, which is acceptable on a bulk straight pad but visible on a premium pad in a transparent retail bag. On a wing fold, ±0.1 mm means the wing tab line is not where the tooling expects it; over a ten-hour run, the fold gradually migrates and your rejection rate creeps up.
The precision number is not about the machine's quality as a whole. It describes the tightest the positioning system can hold over time. Full servo holds ±0.02 mm. If your product tolerances require tighter than ±0.05 mm on any station, semi-servo cannot provide it.
The real question: what stable speed do you actually need?
The real question is not which label appears on the quotation. It is how many pieces per minute your line needs to hold for eight hours to meet your production target.
A full-servo line holds 1000 pcs/min stable. A semi-servo line holds 850-900. A mechanical line holds 750. At a planned daily run of 16 hours with one shift changeover, the difference between 1000 and 850 pcs/min is roughly 144,000 pieces per day — enough to be a meaningful production decision if you are already running at capacity.
But most first lines are not running at capacity. The factory is still learning, operators are still calibrating, raw material changeovers still take longer than planned. A semi-servo line at 850 pcs/min running with high reliability often delivers more output than a full-servo line at 1000 pcs/min running with more rejects and more stops while the team learns the faster line.
The quotation label trap: "full servo" does not always mean every axis
In most cases, a sanitary pad buyer receives a quotation marked "full servo" and assumes every motor on the line is a servo motor. That is not how the industry uses the term. "Full servo" in most quotations means the key stations — core forming, wing former, cutter — carry servo motors. The unwinders may still be vector-drive or frequency-drive. The transport sections may still be cam-driven.
This is not deception. It is an undefined industry term. Two suppliers using "full servo" can be describing meaningfully different architectures, and you will not see the difference until you ask for a station-by-station drive list.
The list you should request before signing: which stations carry their own servo motor, what brand and size, how many axes total, and what drives the rest. If a supplier will not provide that list, the label on the quotation is the full extent of the commitment.
When full servo earns its cost
I believe the specification, not the supplier's label, should drive the configuration decision. Full servo earns its cost when the product asks for it.
A premium ultra-thin winged pad with a precise SAP-dominant core and a retail price that depends on consistent absorbency and appearance earns full servo. The ±0.02 mm positioning keeps the core centred, the wing fold consistent and the line running at 1000 pcs/min stable without the operator chasing drift on the third shift.
A frequent SKU rotation also earns full servo. When the recipe changes multiple times a week — daily pad, overnight, panty liner — the servo re-profiles in seconds instead of requiring mechanical cam adjustments. The changeover time is under 60 minutes on a Welldone full-servo line. On a mechanical line, adding a new size means a mold swap, a cam adjustment and a production trial. The labour and downtime cost accumulates quickly.
When semi-servo is the right call
A standard flat daily pad, produced in one or two sizes, for a market where the product tolerances are wider and the retail channel is price-sensitive — that product does not need ±0.02 mm positioning. It needs reliable output at 850-900 pcs/min, consistent quality within the product's own tolerance band, and a machine the team can maintain without specialized servo technicians.
Semi-servo gives a better capital cost per piece of capacity for that scenario. The machine is simpler to maintain, the drive components are more available locally, and the team learns it faster. That reliability advantage can outweigh the speed advantage of full servo for a first factory in many markets.
Why Welldone
Welldone offers full-servo, semi-servo and mechanical drive options across its sanitary pad, panty liner and menstruation pant lines. The configuration starts from your product specification and production target — see Part 2 of this series, define the product specification before requesting a quote, for the fields that determine which drive architecture your product actually requires.
Station-by-station disclosure
Welldone provides a drive list by station on request, so the quotation describes the architecture, not just the label.
All three configurations
Full-servo, semi-servo and mechanical are all available, sized to your product specification and production volume.
Engineer support
Welldone can provide overseas engineer support for installation, commissioning and training on any configuration.
Conclusion
Full servo and semi servo are not quality tiers. They are architectural choices that match certain products and production volumes. A full-servo line is the right call when the product tolerances require it or when the SKU rotation justifies the recipe management. A semi-servo line is the right call when the product is stable, the range is narrow and the team values reliability over maximum speed.
Before you decide on the label, answer this: which station on your line will be asked to hold the tightest tolerance? Put the servo there. Let the product specification drive the configuration decision, not the other way around.
FAQ
What is the stable speed difference between full servo and semi servo for a sanitary napkin line?
On Welldone's female care lines, a full-servo configuration holds a stable speed of 1000 pcs/min. A semi-servo configuration holds 850-900 pcs/min. The mechanical option holds approximately 750 pcs/min. These figures are from the drive-system specifications on the female care machines page.
Does a full-servo sanitary napkin line really have servo motors on every axis?
The term "full servo" is not standardised across the industry. On Welldone lines, it means independent servo motors for each unwinder and forming station. In other suppliers' quotations, the term may describe fewer servo-driven sections. The reliable way to compare is to request a drive list by station rather than accepting the label alone. See the specification checklist for the fields to confirm before signing.
When does the wing-forming station need to be servo-driven?
Wing forming benefits from servo drive when the pad range includes multiple wing geometries, when the fold angle must be consistent across multiple daily shifts or when size changes are frequent. A servo-driven wing former re-profiles by recipe; a cam-driven one requires a mechanical cam change for each different wing geometry. If you plan to produce more than one or two pad sizes with different wings, servo drive at that station reduces changeover time and reject accumulation.
Is a full-servo sanitary napkin line harder to maintain?
Full-servo lines require technicians who can diagnose servo drive faults and replace drive units. In markets where that skill set is readily available and drive components can be sourced locally, the maintenance burden is manageable. In markets where servo expertise is scarce, a semi-servo or mechanical line may be more practical to support, even if the peak speed is lower. This is worth factoring into the total ownership cost alongside the machine price and production volume.
Tell us your product and production target — we'll confirm which configuration fits
Bring the specification from Part 2 of this series. We will work through the drive architecture with you.
Discuss your configuration See all female care linesWebsite: www.cnwelldone.com Email: welldone@cnwelldone.com