Sanitary Pad vs Panty Liner: Can One Line Make Both? | Welldone

Sanitary Pad vs Panty Liner: Can One Machine Produce Both?
Almost every startup founder in feminine hygiene asks the same question during their first equipment consultation: "Can I buy one machine, run 240 mm winged sanitary pads for three weeks of the month, and switch to panty liners for the last week?"
From a purely mechanical standpoint, the answer is yes. Many stations overlap. But from a manufacturing and financial perspective, sharing one production line across both formats introduces hidden operational frictions that frequently cost more than buying a dedicated liner line.
Starting a Sanitary Napkin Manufacturing Business · Part 4
Part 1: Which line to start with — pad vs liner vs menstruation pant.
Part 2: Define the product first — seven fields before requesting a quote.
Part 3: Full servo vs semi servo — which stations earn independent motors.
Part 4 — this article: can one machine produce both sanitary pads and panty liners?
Part 1: Which line to start with — pad vs liner vs menstruation pant.
Part 2: Define the product first — seven fields before requesting a quote.
Part 3: Full servo vs semi servo — which stations earn independent motors.
Part 4 — this article: can one machine produce both sanitary pads and panty liners?
The co-line question: why buyers want dual capability
Actually, the motivation behind combining sanitary pad and panty liner production on a single chassis is rarely technical curiosity; it is capital preservation and floor-space anxiety. Purchasing one production line requires one footprint, one primary electrical drop, one operator team, and a lower initial capital outlay than buying two separate machines.
For a brand entering a new geographical market, having both daily panty liners (150–180 mm) and daytime winged pads (240–280 mm) allows immediate shelf coverage across retail channels. But a packaging line and a forming chassis designed to handle heavy absorbent fluff pulp behave very differently when asked to run featherweight airlaid paper at high web speeds.
The core structure divergence: fluff drum vs airlaid slit
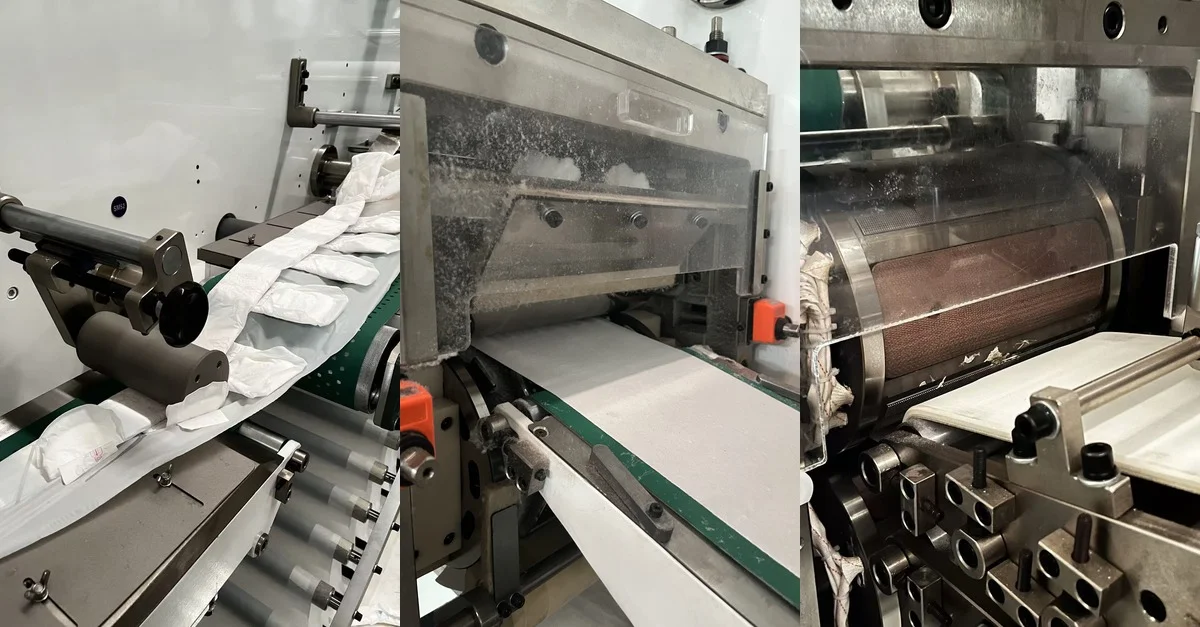
The first major physical divergence between a sanitary pad and a panty liner is how the absorbent core is constructed. A standard daytime sanitary napkin carries a structured core containing fluff pulp and superabsorbent polymer (SAP) weighing anywhere from 6 to 12 grams, formed via a vacuum forming drum.
A panty liner, by contrast, relies on a paper-thin absorbent sheet — typically 40 to 80 gsm airlaid paper or laminated SAP sheet — that requires no pulping, no hammer mill, and no vacuum forming drum. Instead, it only requires an unwinding stand, a tension compensator, and a rotary die slitter.
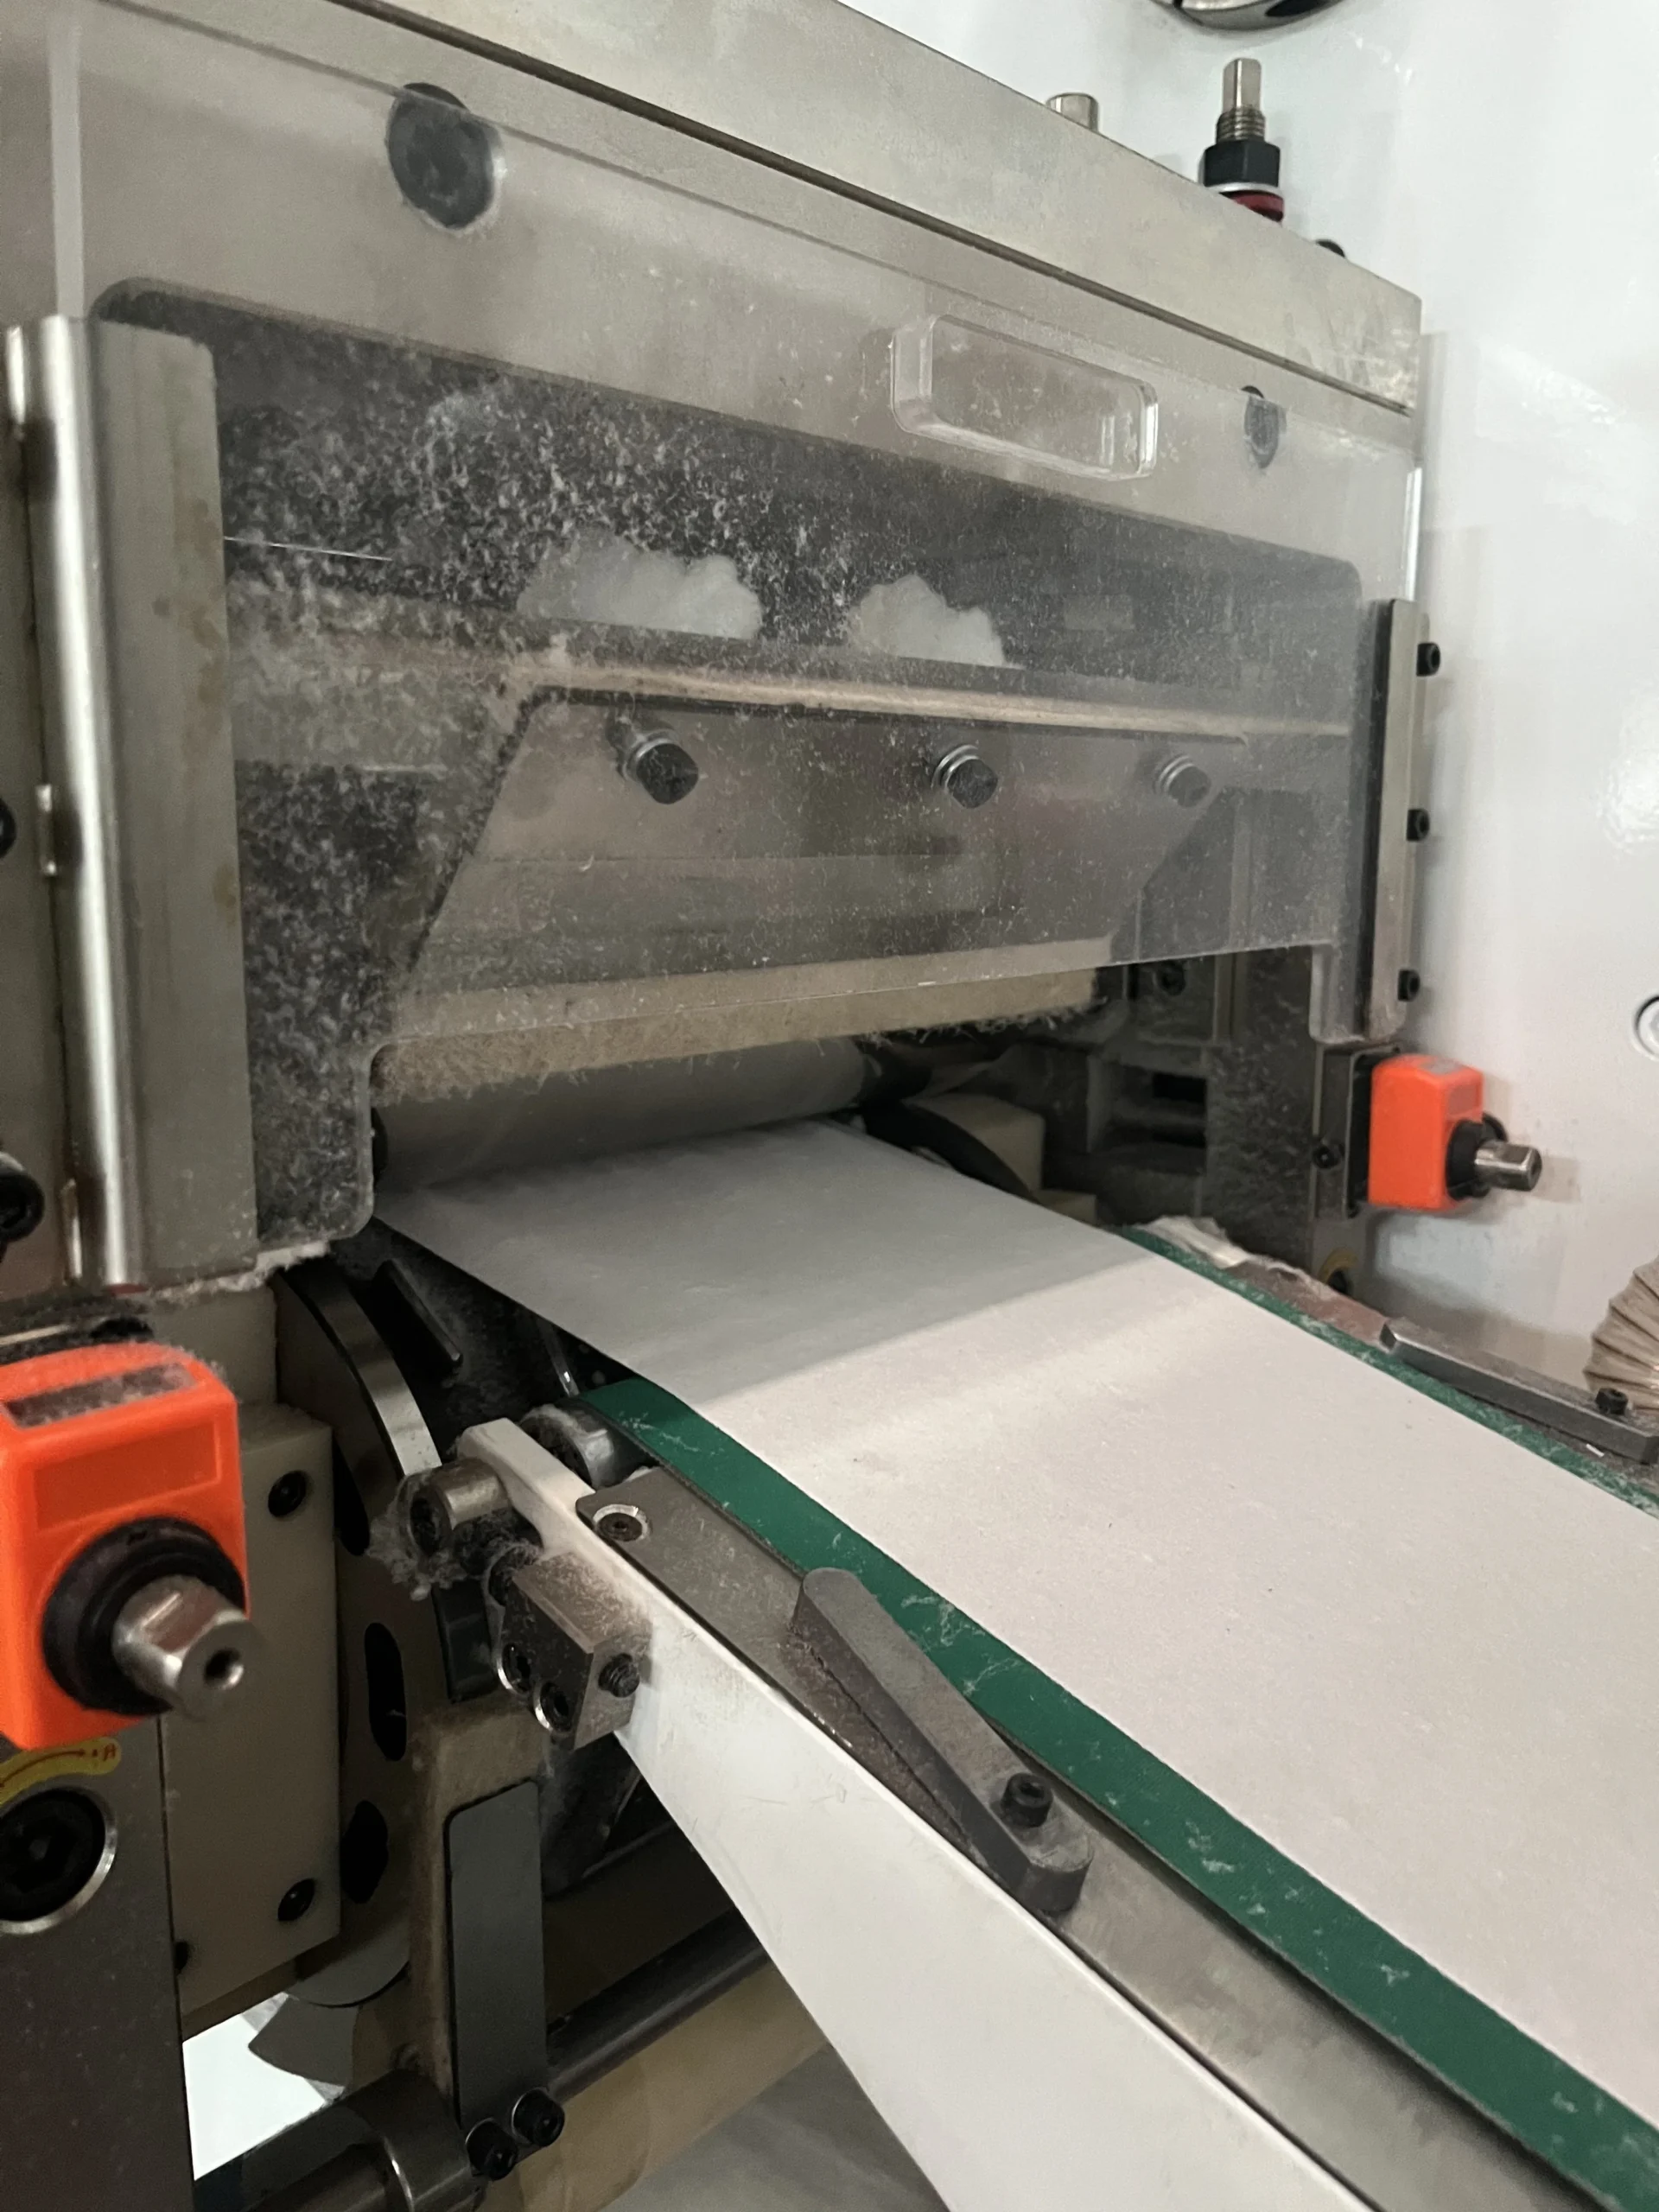
When you combine both on one machine, the bulky hammer mill and fluff forming tower sit completely idle during panty liner runs. You are moving a web across unnecessary idle rollers, multiplying the opportunities for web drift and tension variations on an ultra-light substrate.
The wing station penalty
Over 85% of modern sanitary pads sold globally feature flexible side wings to prevent side leakage and anchor the pad to underwear. Winged sanitary pads require dedicated wing cutting units, adhesive tab applicators, and complex folding guides that flip the wings inward over the top sheet before final perimeter sealing.
Panty liners almost never have wings; they are straight, contoured strips designed for daily light discharge. On a combination machine, when switching from pads to liners, the entire wing folding and wing-tape module must either be disengaged, mechanically bypassed, or physically moved off-line.
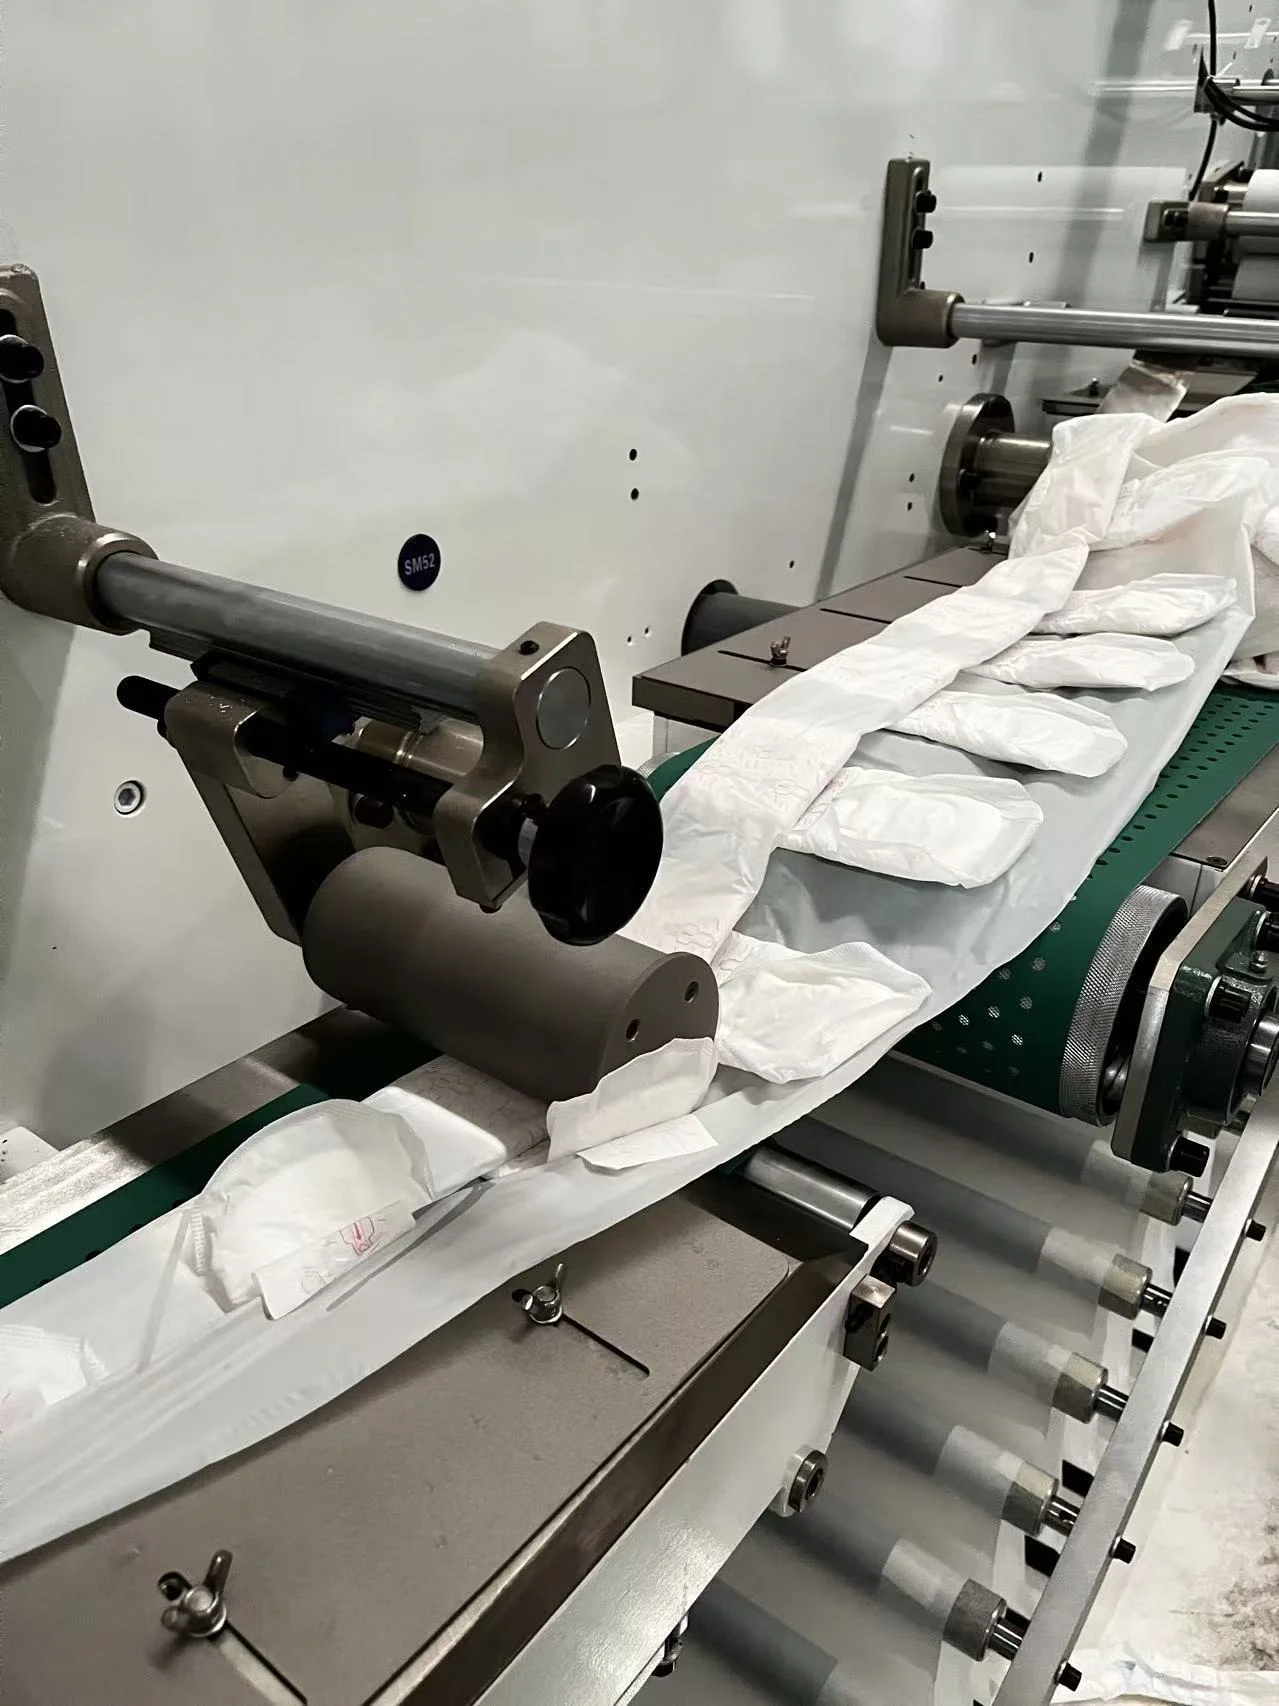
Every bypassed station adds web friction. In high-speed converting, unnecessary roller contacts on light materials increase static electricity and stretch sensitive PE films.
Speed and output compromises
The real question is not whether the machine can make both shapes, but how much speed you sacrifice on the higher-velocity product. A modern dedicated panty liner machine is a lightweight, compact thoroughbred capable of stable production speeds between 1200 and 1600 pieces per minute because it does not carry heavy rotary drums or bulky cutting dies.
Conversely, a standard high-speed sanitary pad machine running winged ultra-thin products typically tops out at a stable speed of 850 to 1000 pieces per minute. When you run panty liners on a heavy-duty sanitary pad chassis, the mechanical inertia of large-diameter rollers and wide-web frame limits your liner speed to roughly 900 to 1000 pieces per minute.
Every minute the combination machine runs panty liners, you are forfeiting 300 to 500 units of potential output compared to a dedicated liner line. Over a week of liner production, that gap adds up to hundreds of thousands of missing units.
Co-line vs dedicated machine comparison
| Dimension | Dual-Purpose Co-Line | Dedicated Separate Lines |
|---|---|---|
| Initial Capital Outlay | Lower (Single base frame + change parts) | Higher (Two complete machine frames) |
| Factory Floor Footprint | Compact (~28 m × 5.5 m total) | Larger (Two bays, ~28 m + ~20 m length) |
| Panty Liner Stable Speed | 800–1000 pcs/min (chassis-constrained) | 1200–1500 pcs/min (dedicated high-speed) |
| Sanitary Pad Stable Speed | 850–1000 pcs/min | 1000–1200 pcs/min |
| Changeover Downtime | 2 to 4 hours per product switch | Zero downtime across product lines |
| Start-Up Material Waste | Higher (Tension and alignment re-tuning) | Minimal (Continuous steady-state tuning) |
| Operator Skill Demand | High (Must master dual web configurations) | Moderate (Repeatable standardized setups) |
The true cost of changeovers: downtime and scrap
In most cases, equipment purchasers budget for the hardware cost of change parts — interchangeable cutting cylinders, forming plates, and packaging guides — but completely overlook the recurring operational penalty of changing over.
Switching a hygiene machine from a winged sanitary pad to an airlaid panty liner is not like changing a recipe on an HMI touch screen. It requires:
- Disengaging or removing the wing cutting and folding assemblies.
- Swapping the perimeter embossing and final contour rotary cutting dies.
- Rethreading the web path from the fluff forming unit to the airlaid unwinder.
- Readjusting hot-melt glue gun positions and spray widths for narrower adhesive coverage.
- Purging and recalibrating the auto-stacker and bag packaging machine.
Even with an experienced engineering crew and full-servo recipe storage, a thorough physical changeover between pads and liners takes 2 to 4 hours. Once the line restarts, running up to 1000 pieces per minute generates hundreds of off-spec scrap products before tension, thermal sealing, and web alignment stabilize. If you switch formats twice a week, you lose 15% to 20% of your weekly production capacity solely to changeover maintenance and scrap recovery.
When to share, when to separate: a decision framework
I believe the decision to choose a combination machine versus dedicated lines should be dictated by your sales volume and order batches, not by your machinery budget.
A co-line machine makes genuine sense if:
- You are launching a startup brand and need to test both pad and liner consumer acceptance before investing in full-scale manufacturing.
- Your distribution model relies on infrequent, large batch runs — for instance, running 20 continuous days of sanitary pads followed by 5 continuous days of panty liners per month.
- Your factory building has strict floor space constraints that make housing two parallel lines impossible.
You should invest in dedicated lines immediately if:
- Your primary sanitary napkin production line already operates at 70% capacity or higher.
- Your market demand requires frequent small-batch deliveries that would force more than one format changeover per week.
- You are serving hyper-competitive, high-volume retail or private-label accounts where panty liner unit production margins depend strictly on achieving 1400+ pcs/min throughput.
Why Welldone
Welldone designs and manufactures high-performance female hygiene equipment, including high-speed sanitary pad lines and dedicated panty liner machines. Whether you require an agile, flexible combination setup or high-throughput standalone lines, Welldone's engineering team provides full turnkey project support — from product specification audits to plant layout design and on-site commissioning.
Turnkey Engineering
Every system is built to your specific absorbent core, topsheet, and packaging geometry rather than generic catalog presets.
Servo Synchronization
Full-servo electronic axis control delivers sub-millimeter registration accuracy and faster mechanical changeovers.
Global Technical Service
Welldone can provide overseas engineer support for installation, commissioning and training.
Conclusion
Can one machine produce both sanitary pads and panty liners? Yes. But the true question is whether your business model can afford the speed reduction, the changeover downtime, and the operational complexity that dual capability demands.
Before specifying a combination machine, calculate your monthly unit demand and changeover frequency. If changeover stops will consume more than two shifts per week, separating your investments into two dedicated lines will always deliver a faster payback and a smoother production floor.
FAQ
Can an existing sanitary napkin machine be upgraded to produce panty liners?
Yes, if the machine chassis has adequate space to mount an airlaid unwinder, an auxiliary web guide, and interchangeable rotary cutting dies. However, retrofitting an older mechanical machine can be cost-prohibitive compared to investing in a modern compact panty liner machine.
How long does a complete changeover between pads and liners take?
On a modern full-servo machine with quick-release tool holders and stored HMI recipes, a mechanical changeover typically takes 2 to 3 hours. On semi-servo or mechanical lines, changing cutting cylinders, bypassing wing units, and manually tuning tension can require 4 to 6 hours.
Why do panty liners run faster on dedicated machines than on combination lines?
Dedicated panty liner machines feature small-diameter rotary cutting cylinders, compact web paths, and lightweight frame inertia. Combination lines carry heavy drum assemblies and wider conveyor beds designed for 300+ mm pads, which introduce mechanical vibration and dynamic web drag at speeds exceeding 1000 pcs/min. Check our female care machines overview for exact speed ratings.
What raw materials can be shared between sanitary pads and panty liners?
Both products frequently share the nonwoven topsheet, polyethylene (PE) film backsheet, hot-melt construction adhesives, positioning adhesive, and siliconized release paper. However, the absorbent core materials differ completely: pads use fluff pulp rolls and SAP granules, while liners use pre-formed airlaid paper rolls. See our specification checklist for raw material planning.
Planning your female care production floor?
Contact Welldone's engineering specialists to evaluate whether a flexible combination setup or dedicated production lines fit your regional market demand.
Request Project Consultation Explore Female Care EquipmentWebsite: www.cnwelldone.com Email: welldone@cnwelldone.com